
Why Hot Runner Maintenance Cycles Should Not Be Calendar-Based
工艺参数16 min read
On this page
"Maintenance every six months" is the most common yet least reliable guideline. Wear varies significantly between 10,000 and 100,000 cycles within that period.
Maintenance intervals should be based on "actual usage conditions," not time.
Calculation Basis
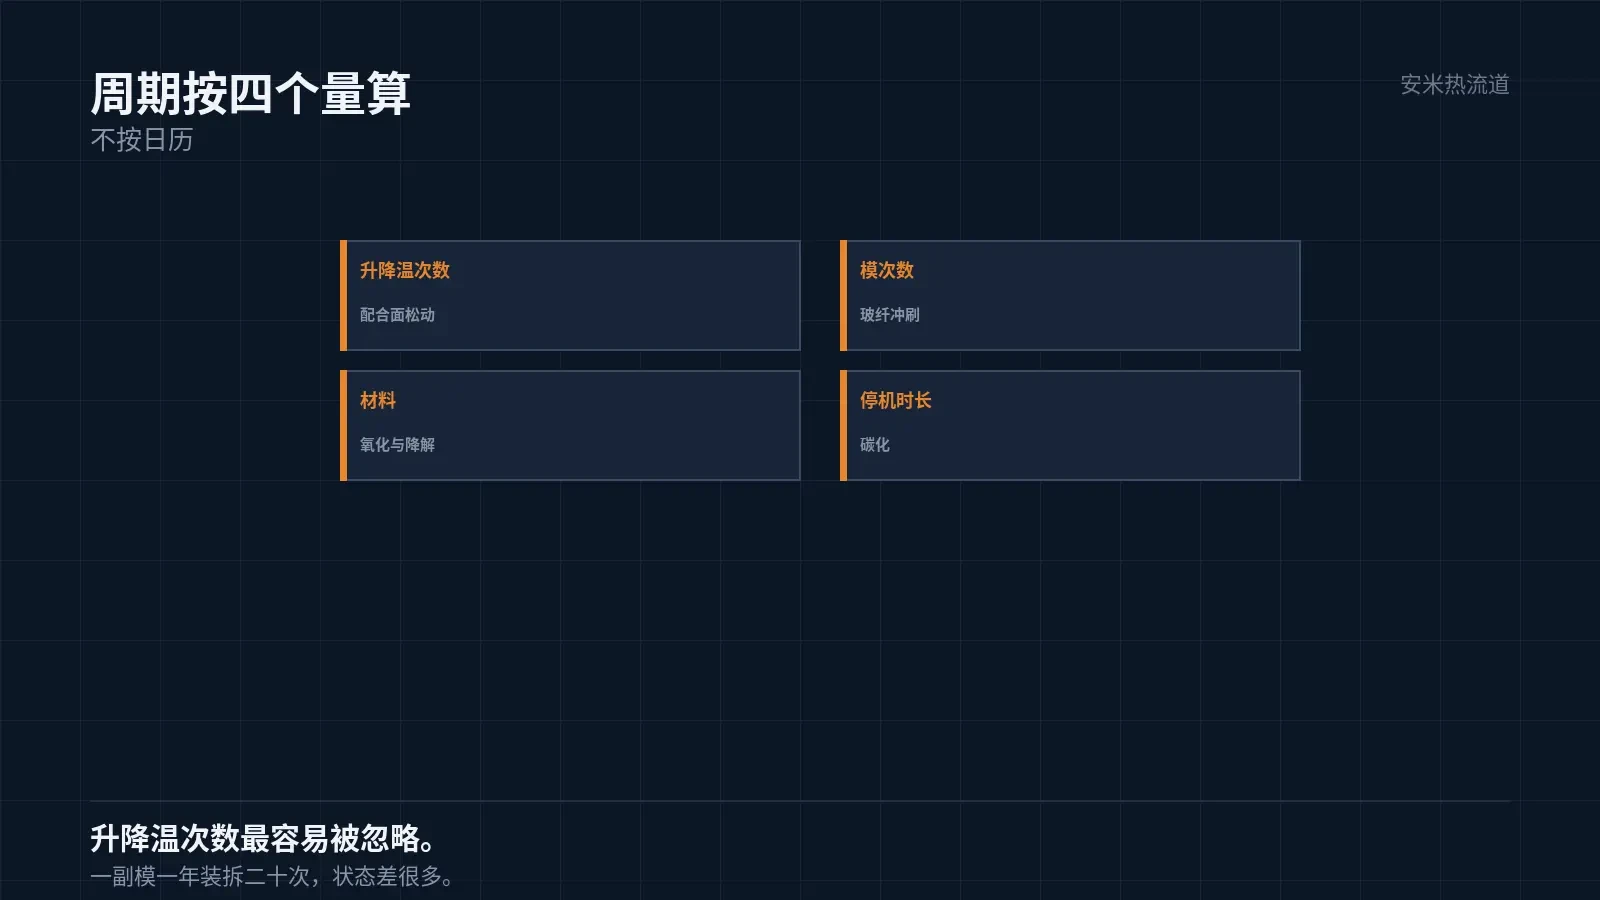
The first factor is "thermal cycling count." Expansion and contraction cycles are the primary cause of loosening at mating surfaces.
The second factor is "shot count." Higher shot counts accelerate wear, especially from abrasion caused by glass-filled materials.
The third factor is "material." High glass-fiber content accelerates wear, while high-temperature materials increase the risk of oxidation and degradation.
The fourth factor is "downtime duration." Prolonged downtime causes material carbonization in runners, necessitating a purge upon restart.
Among these four factors, thermal cycling is often overlooked. A mold installed and removed 20 times per year differs significantly in condition from one handled only twice.
Maintenance Checklist
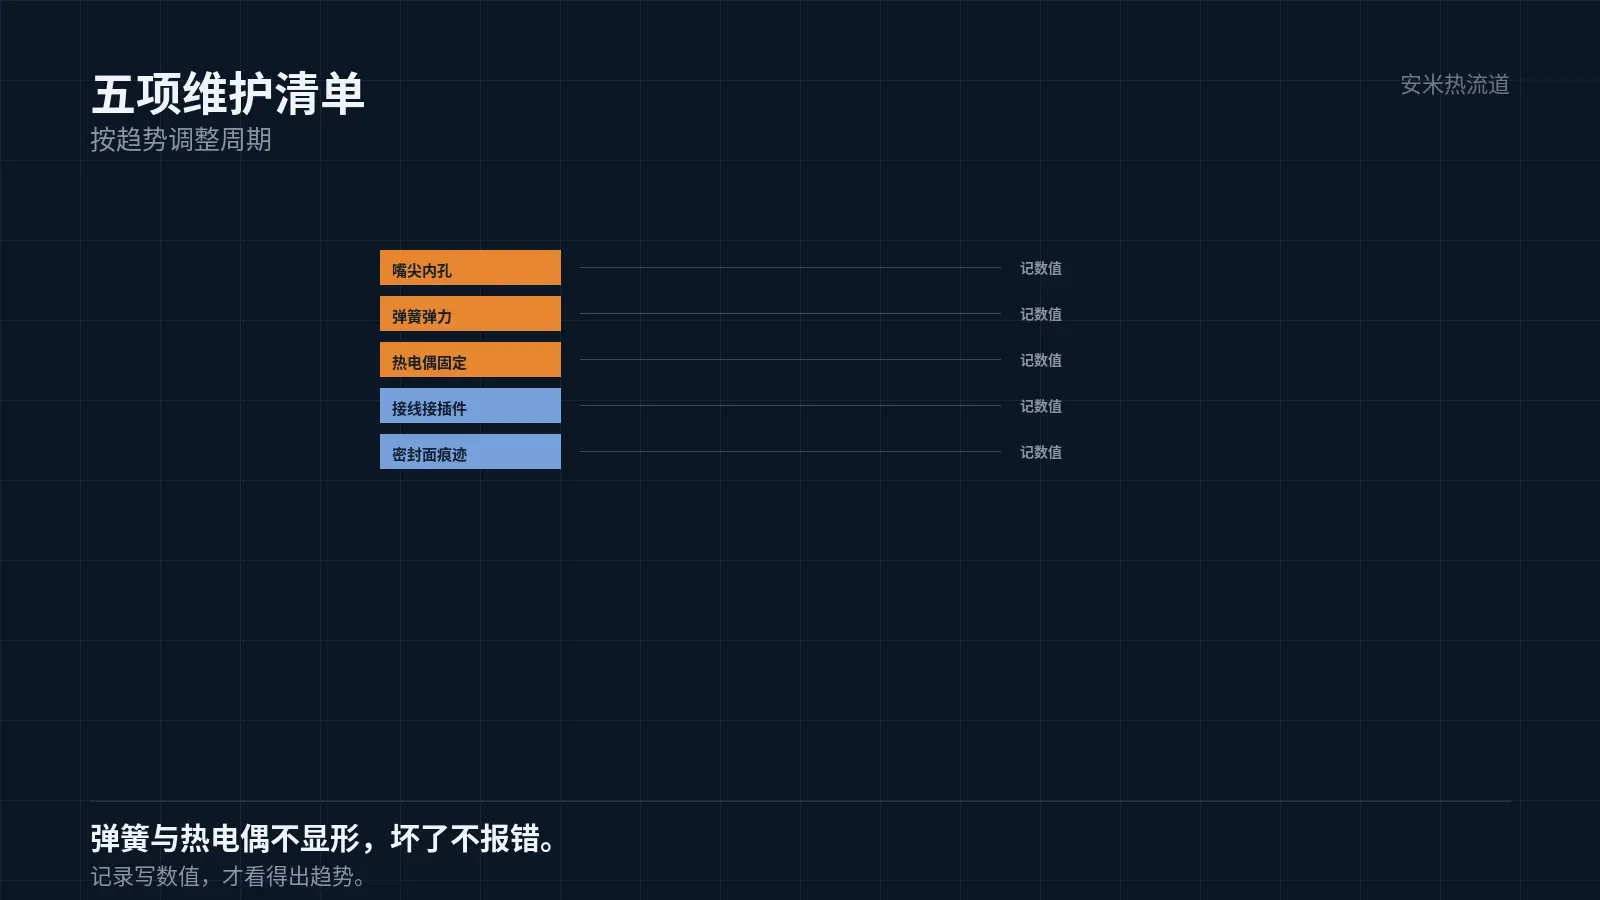
Item 1: Nozzle Tip. Inspect bore diameter, surface wear, and material buildup. An enlarged bore causes a larger gate mark.
Item 2: Spring. Measure free length and force against new parts. A relaxed spring reduces compensation capability.
Item 3: Thermocouple. Verify mounting security and reading accuracy. Loose thermocouples cause signal drift.
Item 4: Wiring and connectors. Inspect for oxidation or looseness. Poor contact can cause temperature fluctuations.
Item 5: Sealing surfaces. Check for uniform contact marks and worn grooves.
Of the five items, springs and thermocouples are most easily overlooked. They show no visible signs of failure and do not trigger error codes.
Determine Maintenance Intervals
The initial cycle can be set to a conservative value, such as inspection every 5,000 shots or every 10 temperature cycles.
Then adjust based on actual records: extend the interval for items with no anomalies, and shorten it for those with anomalies.
Adjustments are based on trends, not isolated incidents. Shorten the interval if an item deteriorates across three consecutive checks.
This is the core of preventive maintenance: monitor trends, not just current status. Normal readings today may mask worsening conditions.
Maintenance records must include "numerical values," not just "normal." Numerical values are required to identify trends.
Numerical records must follow consistent standards—same location, tool, and method. Changing standards breaks trend continuity.
Therefore, specify "where to measure" and "which tool to use" in the maintenance checklist. Clear specifications ensure continuity during personnel changes.
This point may seem minor, but it determines whether the maintenance system can operate long-term.
Another key aspect of maintenance is "who performs it." Assign fixed personnel, schedules, and forms; do not rely on ad-hoc availability.
Fixed personnel accumulate experience. With rotating staff, forms are completed, but decisions remain guesswork.
In the maintenance system, people come first. Forms are tools to support users—not replace them.
Small workshops often overlook this, leading to forms without judgment and turning maintenance into a mere formality.
The third key to maintenance is spare parts. Wear items must be stocked for immediate replacement without waiting for procurement.
Spare part lists should be based on replacement frequency. Nozzle tips, springs, and thermocouples are high-frequency items.
Inventory levels don't need to be high, but stockouts must be avoided. A single stockout causes production downtime losses far exceeding inventory costs.
This is especially critical for high-temperature applications. PEEK nozzle tips have long lead times; without stock, delays occur.
Proper storage of spare parts is essential. Springs are prone to rust, thermocouples can bend, and nozzle tips may suffer impact damage; all require individual packaging.
Improperly stored spare parts may perform differently than new ones upon installation. This is especially critical in high-precision applications.
Rotate spare parts inventory regularly: replace items past their shelf life. Using aged parts complicates troubleshooting.
Shelf life varies by material and packaging. Rubber components and springs have shorter lifespans than metal parts. Set a limit for each item in the list.
Expiration does not mean failure; re-inspection is required. If it passes, continue use; otherwise, replace.
Major and Minor Overhauls
Minor overhaul includes inspection, cleaning, and tightening. It requires no production downtime and is completed in half a day.
Major overhaul requires disassembly, replacement of worn parts, and re-measurement. It necessitates machine downtime and takes one to three days.
Major overhauls are typically triggered by anomalies detected during minor overhauls, declining part quality, or reaching the preset shot count limit.
Post-major-overhaul verification includes four steps: cold-state inspection, heat-up re-check, dry cycle injection, and trial molding.
Skipping post-overhaul verification shifts risk to mass production. This step is often omitted on-site.
Additional Items for High-Temperature Solutions
PEEK solutions require an additional check: heater resistance values. Heaters degrade quickly at high temperatures, with resistance changes serving as indicators.
PPS solutions require an additional check for mold temperature uniformity. At 150°C, zone-to-zone variations increase with usage time.
The PA46 solution requires an extra step: barrel cleaning. The processing window is narrow, and residual material has a greater impact than with low-temperature materials.
These additional items are due to "material sensitivities." Maintenance checklists must be customized by material; a single generic table cannot be used.
Send us the material, shot count, heat-up/cool-down cycles, and current maintenance method. We'll review it against the system and provide a quote upon confirmation.
MATCHED BY MATERIAL AND DEFECT
This article covers stringing, drooling, clogging, and high-heat resins; refer to SD for gate freeze and break-off.
Register for a selection review and quote
Submit part, mold, and material details. Our engineers will evaluate the gate solution per part and provide a quote.
Upload a 2D layout drawing using the form.
Online selection and quote
Scan to register