AM Industry FHFC logo
AM Industry Rapid Heat and Rapid Cool Four-Point Hot Runner

Fast Heat Fast Cool Hot Runner:Dynamic Gate Temperature

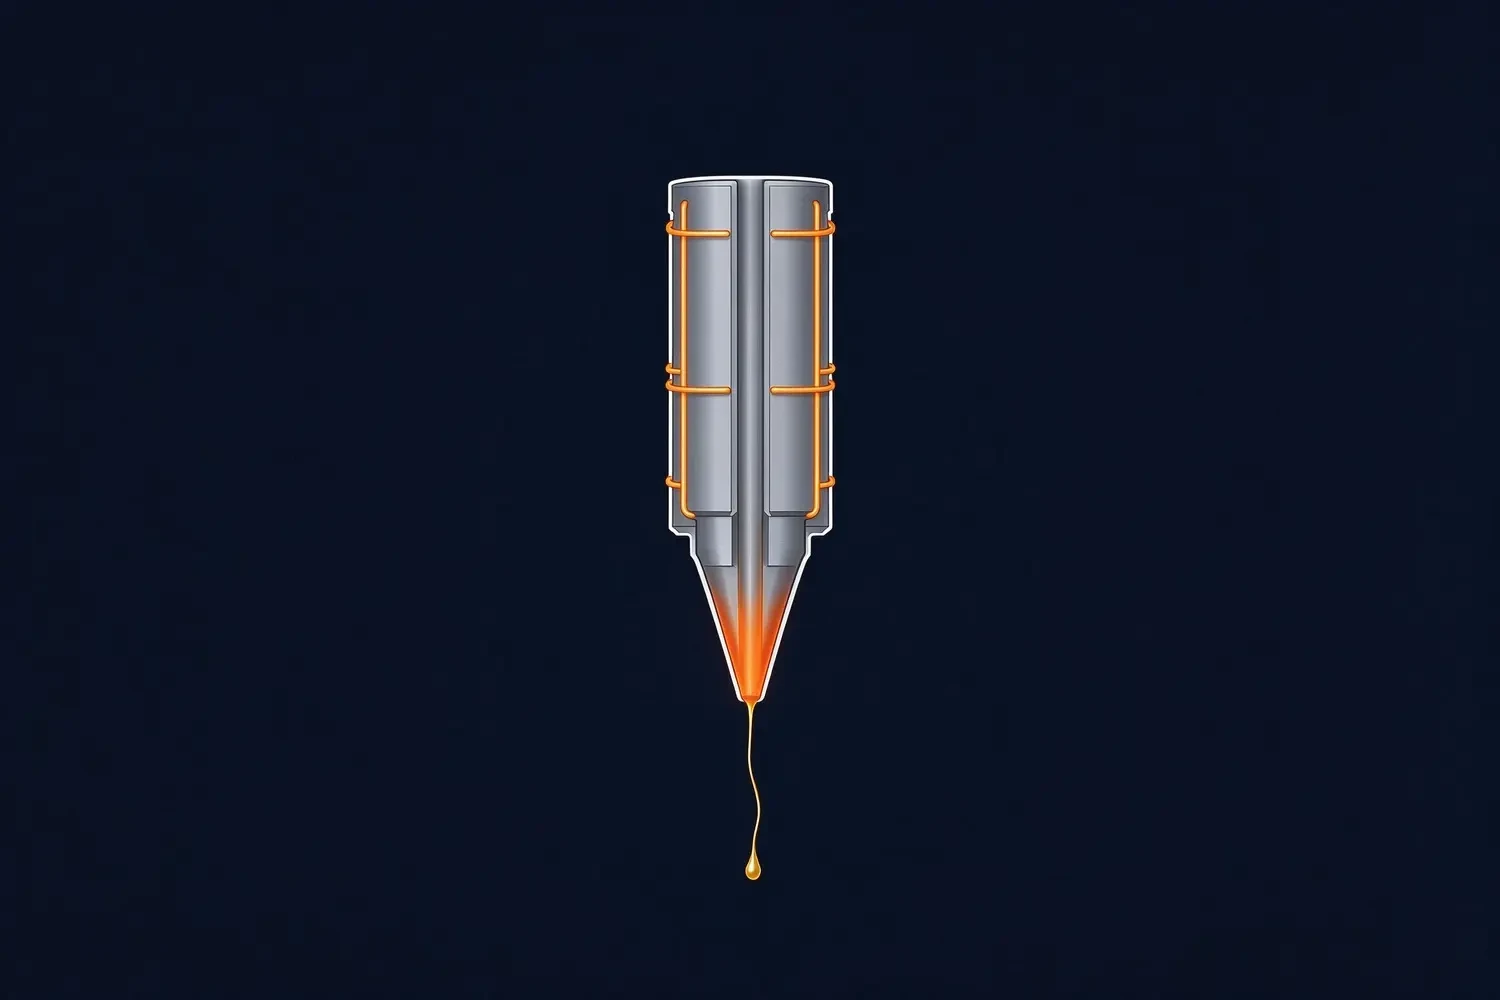
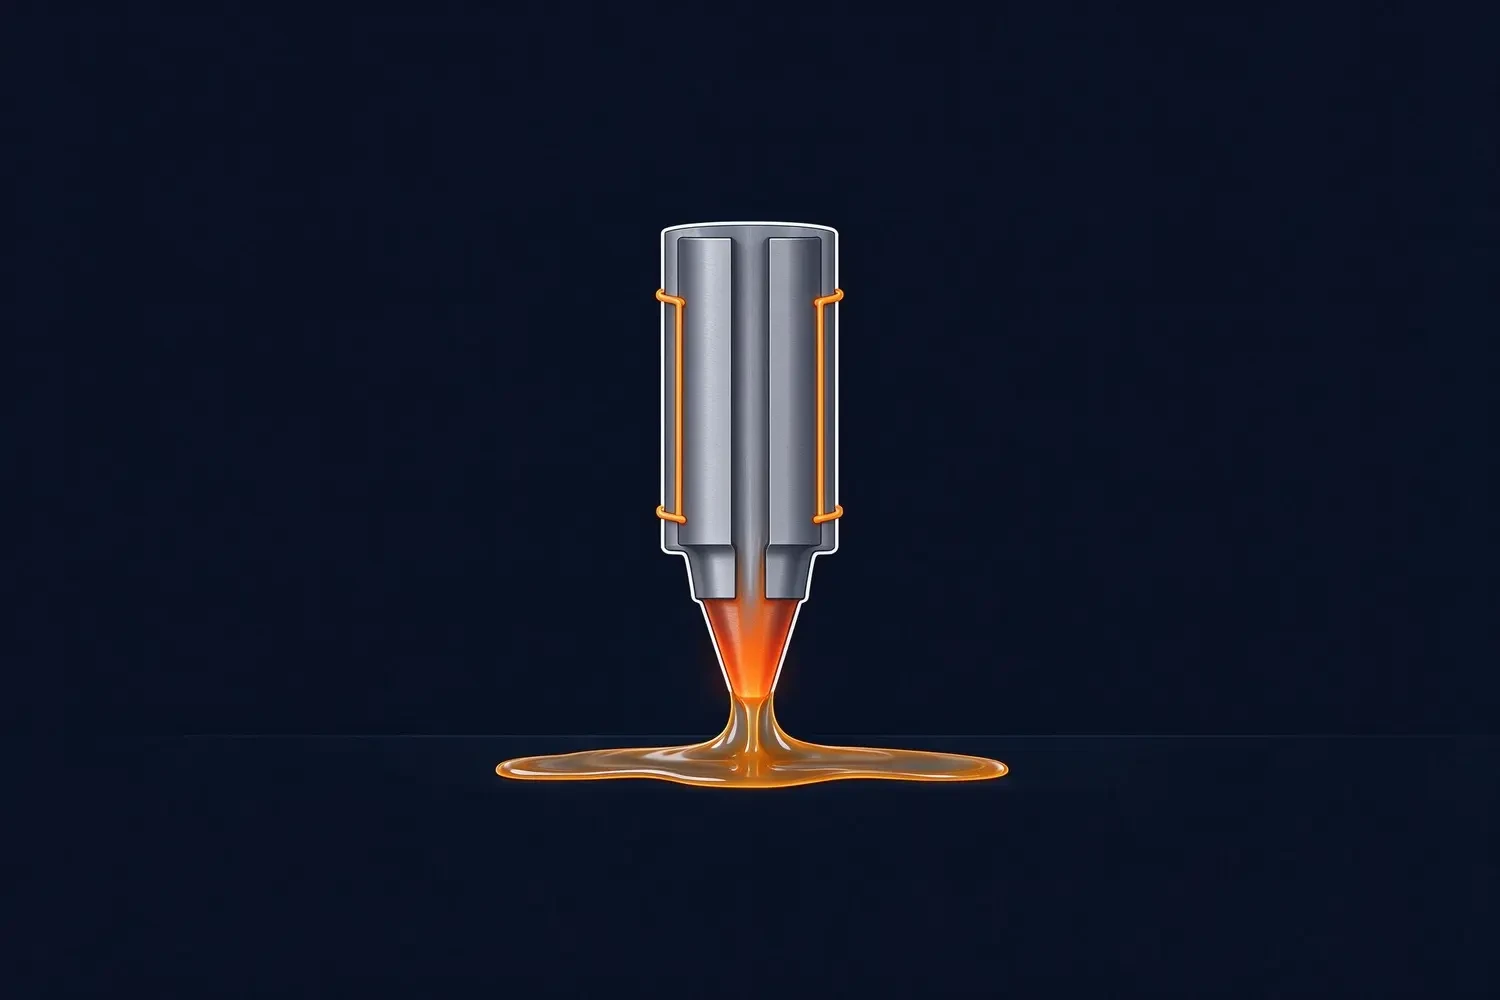
An independent temperature loop at the gate switches setpoints across filling, packing, and cooling stages, then freezes the gate to break the melt before mold opening.

7 filed patent applications

Invention, Utility Model, and Design

Shenzhen proposal · Dongguan build

Design, assembly, and powered testing

4 nozzle series

Gating and gate mark comparison

39 defect solutions

Verified across six process links

Sealing and corrosion resistance

Highly filled and corrosive resins won't corrode the nozzle or leak at the seal.

Lower pressure drop

Reduces the risk of degradation from trapped frictional heat.

Machining tolerance compensation

The nozzle face seals tightly against the manifold to prevent leakage and seepage.

No blind spots

Rounded transitions leave no residue, reduce pressure drop, and balance every channel.

TECHNOLOGY

Dynamic gate temperature, how it works

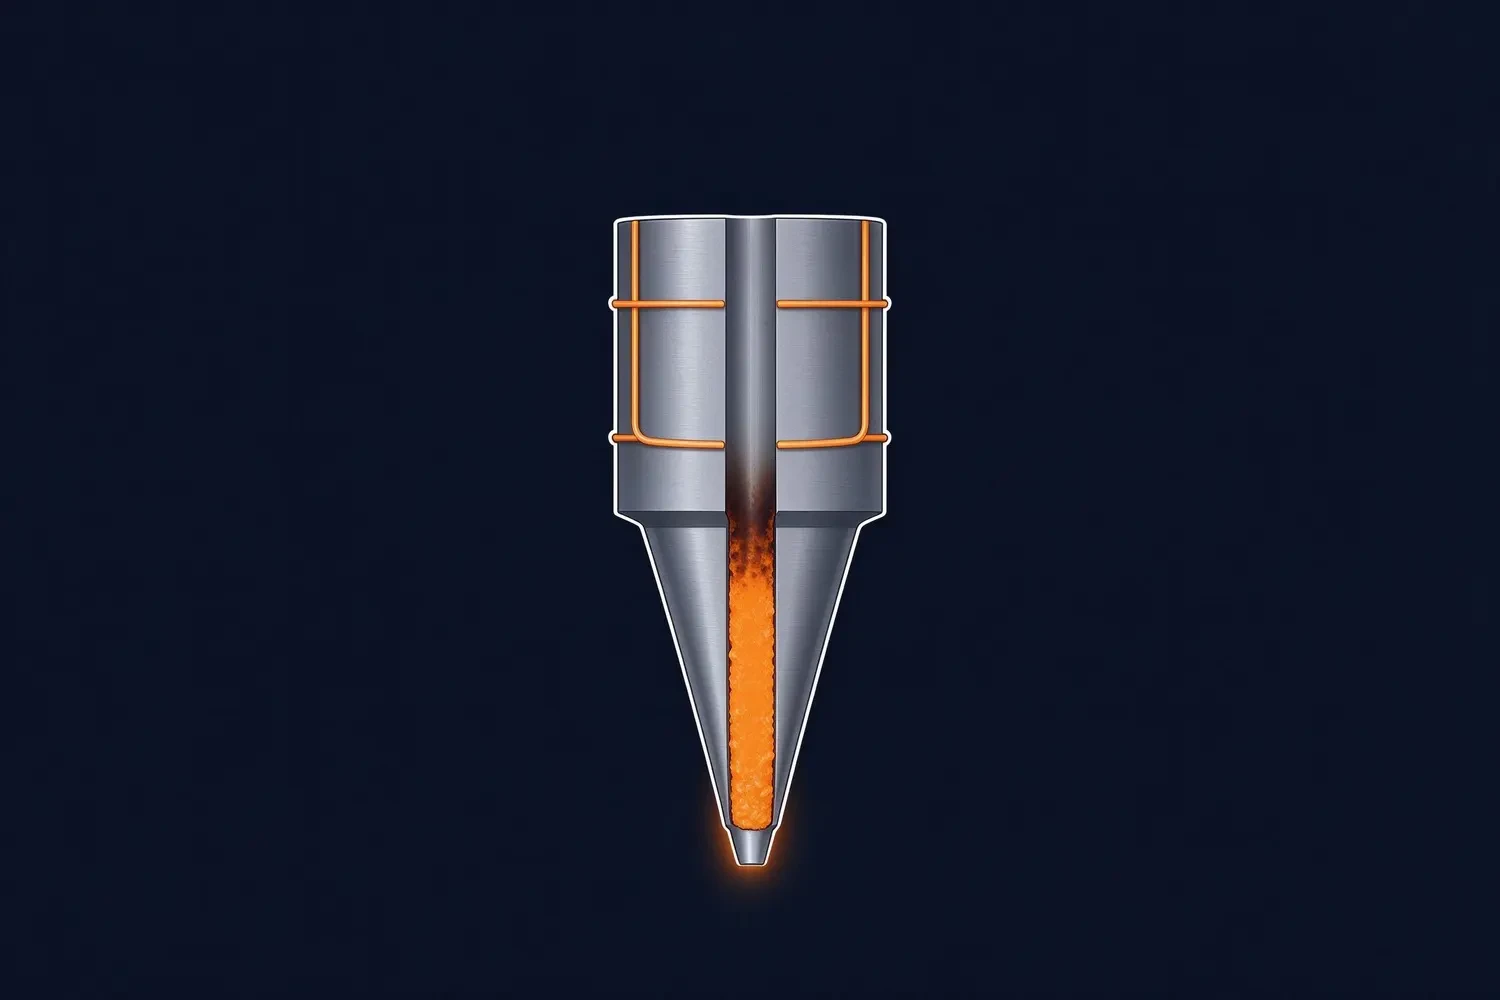
The whole runner does not heat and cool. Temperature changes only at the tip and gate, switched within one molding cycle.

Manifold (constant)Nozzle bodyDynamic zoneTip to gateRunner mid-section constantGate end

01 / Heating scope

Tip only

Dynamic temperature applies only to the tip section

The tip is heated and measured independently, with temperature cycling at the tip. The manifold and nozzle body stay on the constant-temperature controller, so the mid-runner does not follow the cycle.

Dynamic zone = tip to gate
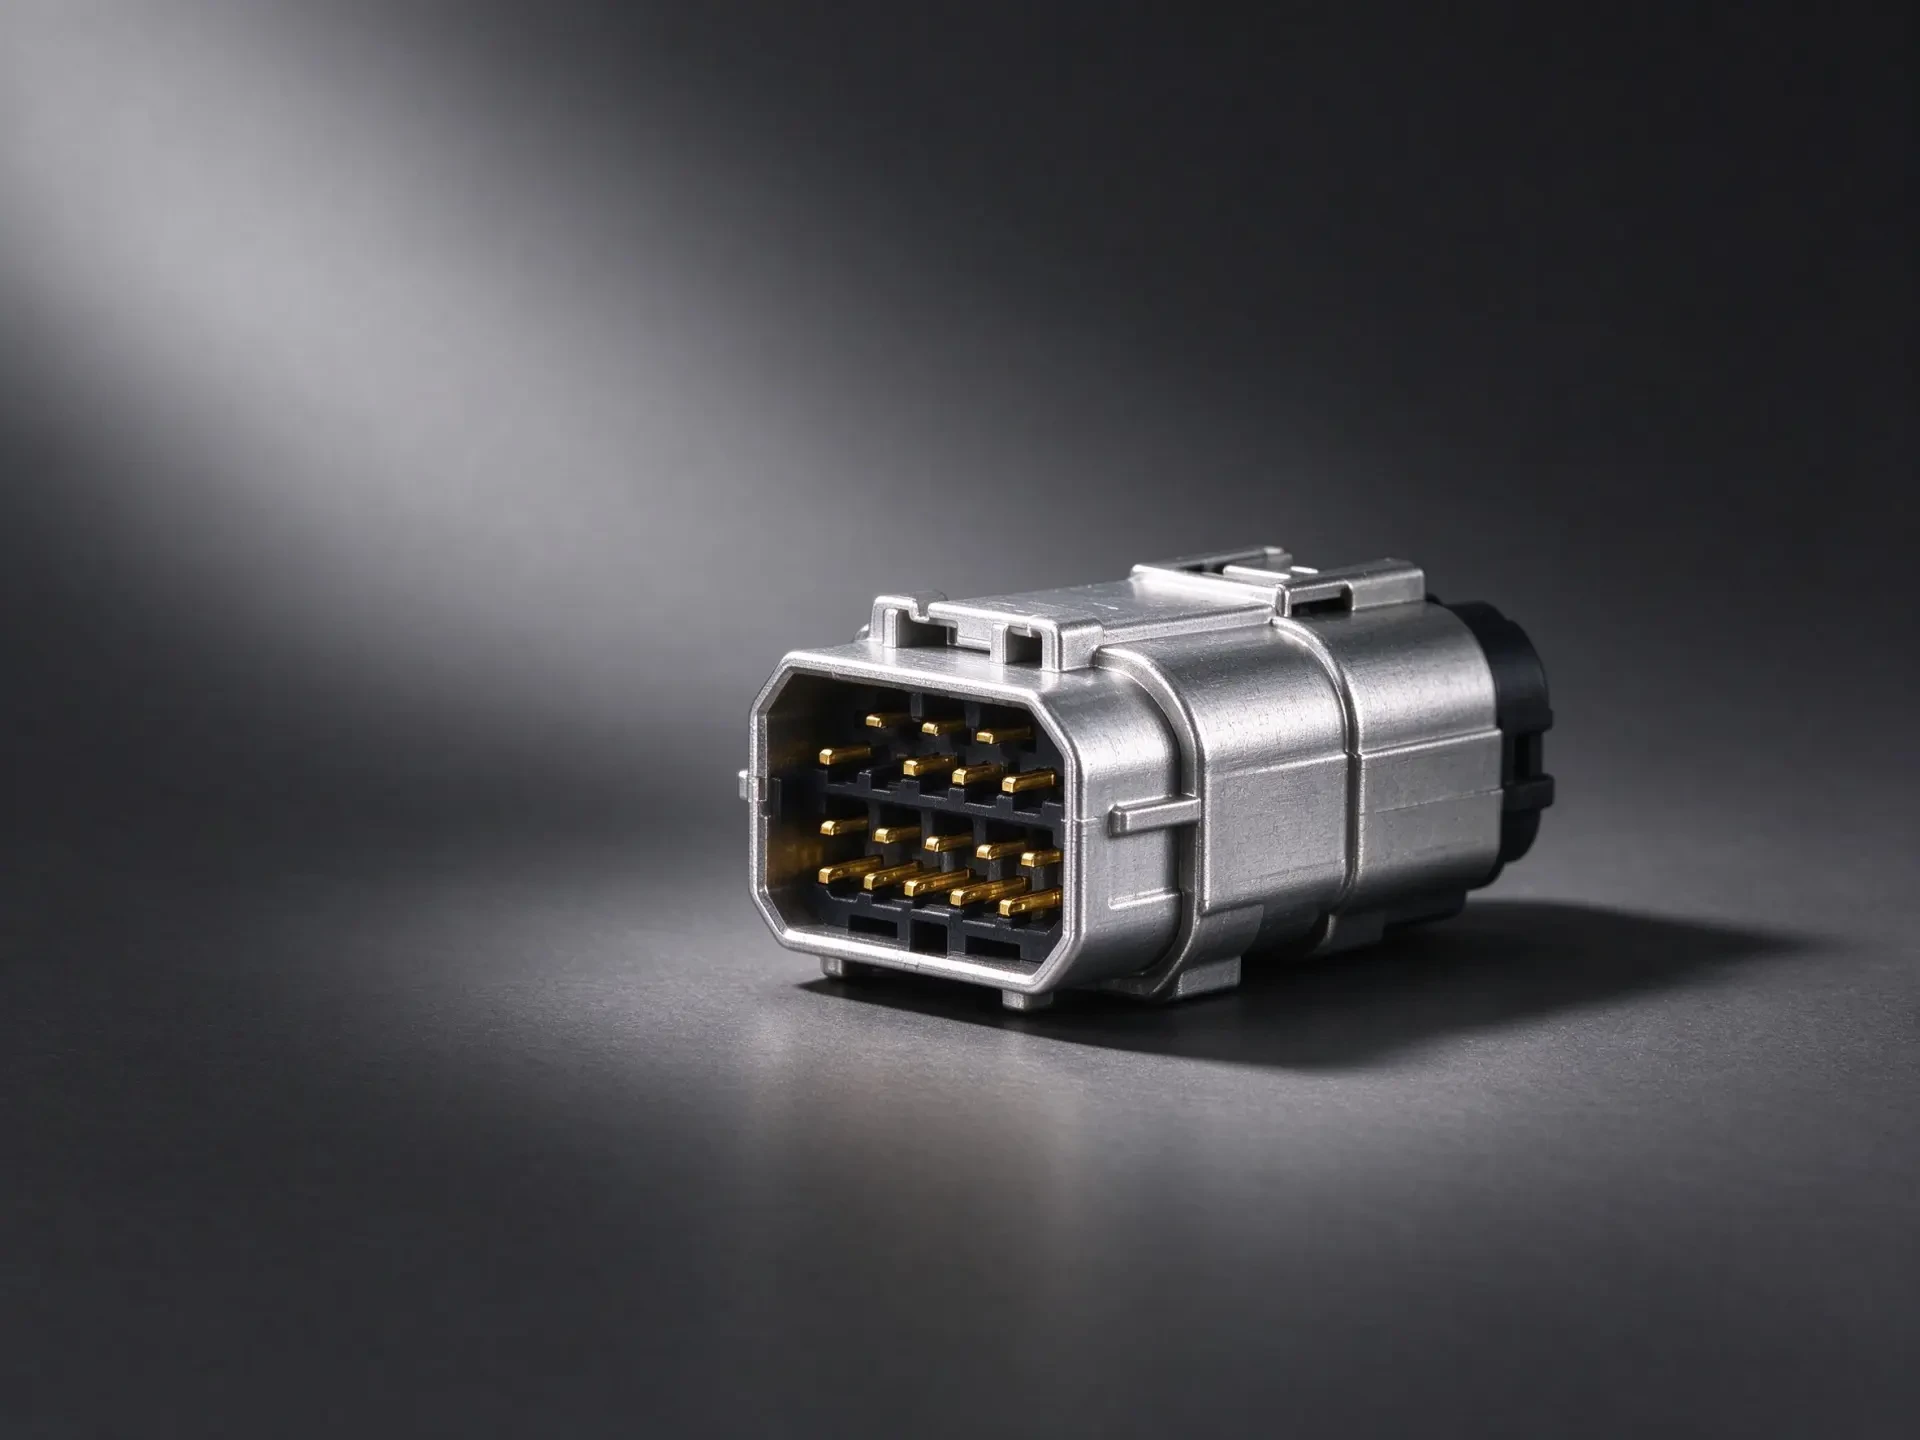
TempTime320℃260℃FillPackageCool

02 / Cycle sequence

Fill → Pack → Cool

Three temperature stages in one cycle

The fill stage rises to the set temperature (320℃ in this example) for flow, packing holds it, and cooling drops to 260℃ so the gate solidifies before the cavity.

Values are examples; set them by material
ManifoldNozzleGate solidifiedGate breakCooling stage

03 / Break-off

Breaks on mold opening

Break-off comes from gate solidification

The cooling stage drops the gate below the material's solidification temperature, sealing the channel so the sprue breaks at the gate when the mold opens. SD Series (SD, TP) work this way; valve gates (VG, PVG) close with a pin.

Solidified break-off without sacrificing cycle time

FROM DESIGN TO VALIDATION

From drawing to on-machine validation: a proposal in 2 days, delivery in 20–25 working days

Send part drawings, material grade, mold layout and molding conditions; we issue the proposal from the layout. Once approved, the order is placed, the assembly is completed in Dongguan and shipped to site, where our staff support installation and on-machine validation.

01

Requirement review

Same day

Send part drawings, material grade, mold layout, cavity count and molding conditions; once complete, a feasibility judgement is issued the same day.

02

Proposal design

2 working days, 1–2 days joint review

The layout defines runner routing, nozzle type and temperature control; drawings are then reviewed with the customer's mold engineer until the tool is ready to open.

03

Precision manufacturing

20–25 working days

After order confirmation, material is cut, machined, assembled and powered up; every channel is temperature-verified before the assembly ships.

04

On-site on-machine validation

Half a working day

We install and wire the system on site, support parameter tuning and hand over once consecutive parts run stable.

Lead times above apply to standard molds and operating conditions with imported parts arriving on schedule. If imported parts are short or a customer specifies a brand, lead time is quoted separately.

Proposals and commercial work are handled in Shenzhen; machining and assembly in Dongguan; the assembled system then ships to the customer site.

Gate problem?

Register the basic project details. Our engineers will review the part, mold and material, then provide a proposal and quotation.