
Why do molds and screws wear out faster when processing high glass fiber materials?
工艺参数16 min read
On this page
Using the same mold, standard material produces 1 million shots, but glass-filled material causes issues after 300,000 shots. Symptoms include enlarged gates, runner wear, and degraded part appearance.
This is not a mold quality issue; it results from the abrasiveness of glass fiber. This article analyzes the associated cost.
Fiberglass Hardness
Glass fiber hardness exceeds that of the mold steel matrix. As the melt flows at high speed, glass fibers abrade surfaces like sandpaper.
The gate undergoes the most severe wear. Due to its small cross-sectional area and high flow velocity, abrasion occurs fastest here.
As the gate wears larger, flow rate increases, gate vestige grows, and multi-cavity balance is disrupted.
Runner wear is secondary. With larger diameters and lower flow velocities, wear occurs more slowly but becomes apparent over time.
The inner walls of the hot runner are also wear points. High-speed flow of material with high glass-fiber content affects both the runner walls and valve pins.
Therefore, hot runners for high glass-fiber materials require wear-resistant components, and valve pin clearances must include wear allowances.
Screw and barrel wear follows this pattern: the screw flight, check ring, and barrel inner wall are all wear points.
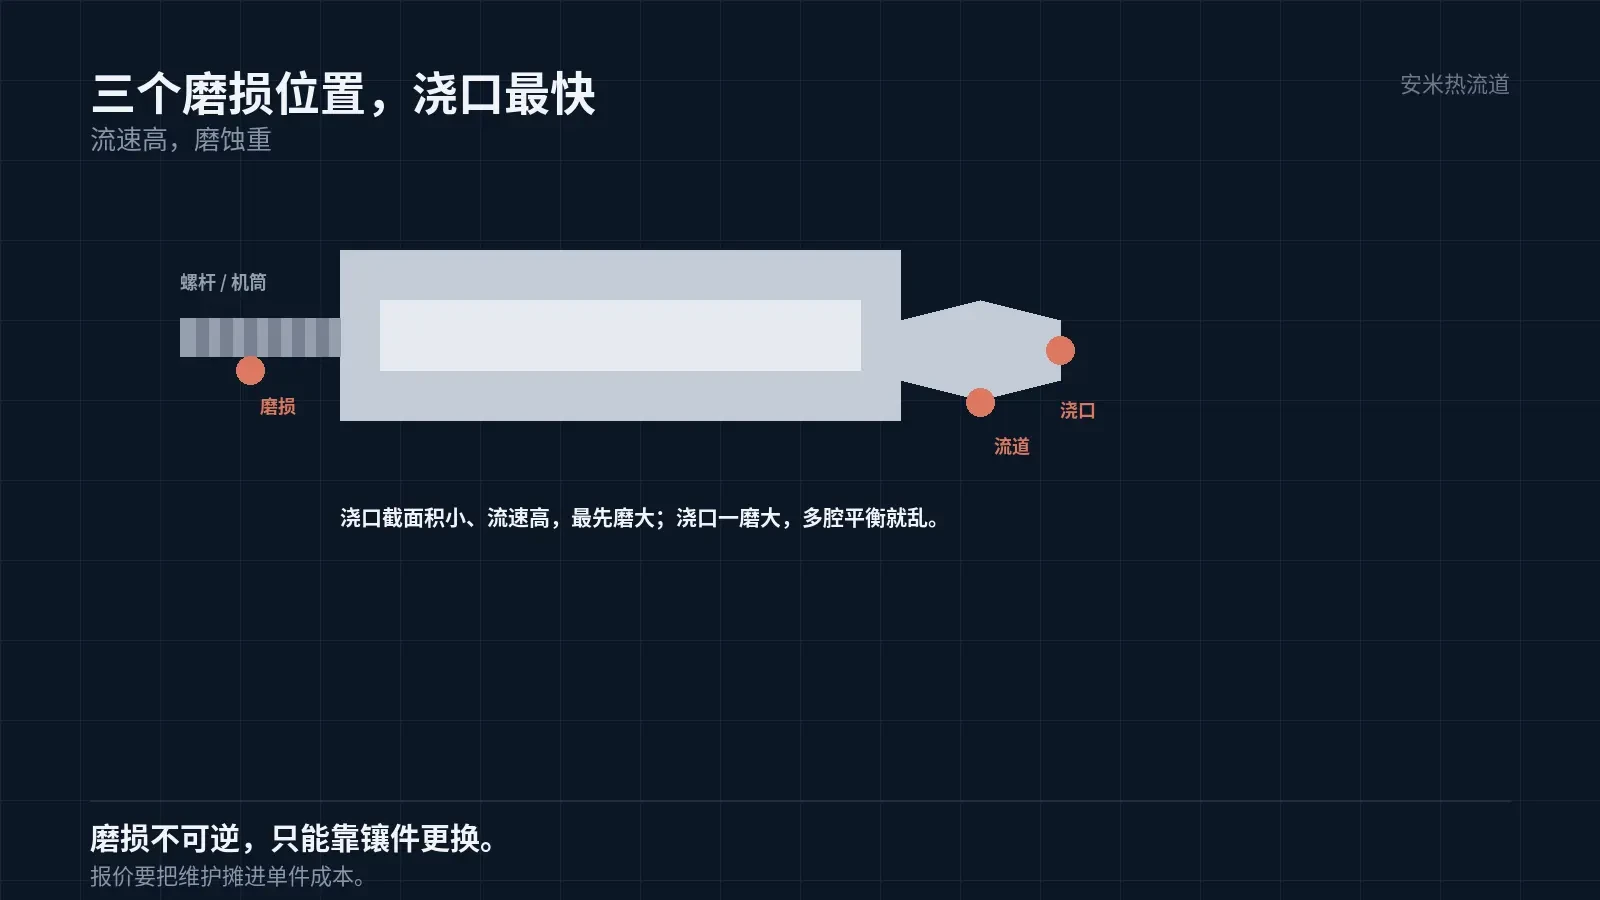
Wear effects develop progressively.
Initially, parts meet specifications. After tens of thousands of shots, the gate enlarges, flash increases, and cosmetic defects appear.
After tens of thousands of additional shots, multi-cavity balance is lost, weight variation between cavities increases, and dimensional tolerances are exceeded.
Parameter adjustments can partially compensate at this stage but cannot fully restore performance, as wear is irreversible.
Therefore, molds for high-glass-fiber materials require a "wear budget": define inspection intervals and gate insert replacement schedules.
Wear also alters flow behavior. An enlarged gate increases flow rate, leading to higher part weight in that cavity and disrupting multi-cavity balance.
Therefore, gate inserts in multi-cavity molds must be individually replaceable. Replacing the entire mold set is too costly.
This budget must be included in all quotations. If customers compare only unit price instead of service life, the supplier will ultimately incur the loss.
Calculation method: Estimate lifespan based on shot count and amortize insert replacement, downtime, and mold repair costs per part. This value often exceeds the material price difference.
Bundle the unit price and maintenance costs in a single quote to ensure client clarity. Quoting only the unit price can lead to future disputes.
Another consideration: spare parts. For molds processing high-glass-fiber materials, maintain multiple sets of gate inserts in stock. Ordering after failure leads to costly downtime.
Set spare part inventory based on wear rate: stock more for fast-wearing components, less for slow-wearing ones.
Gate insert replacement must comply with standards. Verify part weight and gate dimensions after replacement; skipping this step renders the replacement ineffective.
Maintain records for insert replacements: shot count, part weight variation, and wear on removed inserts. Three records enable lifespan calculation.
Mold storage requires attention. Gates in long-idle molds may rust, causing molded parts to fail cosmetic inspection.
How to Reduce Wear
First, select the right mold steel. Use H13 or S136 for high-glass-fiber materials; heat treatment must exceed HRC 50.
Second, surface treatment. Nitriding, chrome plating, and PVD coatings enhance wear resistance. Coatings must be uniform to prevent localized spalling.
Third, use an insert for the gate. Replace the worn insert instead of the entire mold. This decision must be made during mold design.
Fourth, use rounded corners in runners. Sharp corners cause high flow velocity and rapid wear; rounded corners smooth the flow.
Fifth, select wear-resistant screw and barrel types. Bimetal screws and tungsten carbide coatings are common options.
All five measures deliver significant cost savings with minimal investment. Neglecting them will result in higher maintenance and downtime costs down the line.
Another often-overlooked factor is material drying. Glass-filled materials absorb moisture; water vapor in the melt accelerates degradation and changes abrasiveness.
High glass-fiber content material that isn't dried sufficiently causes rough part surfaces and accelerated mold wear. Pay special attention to this in southern workshops.
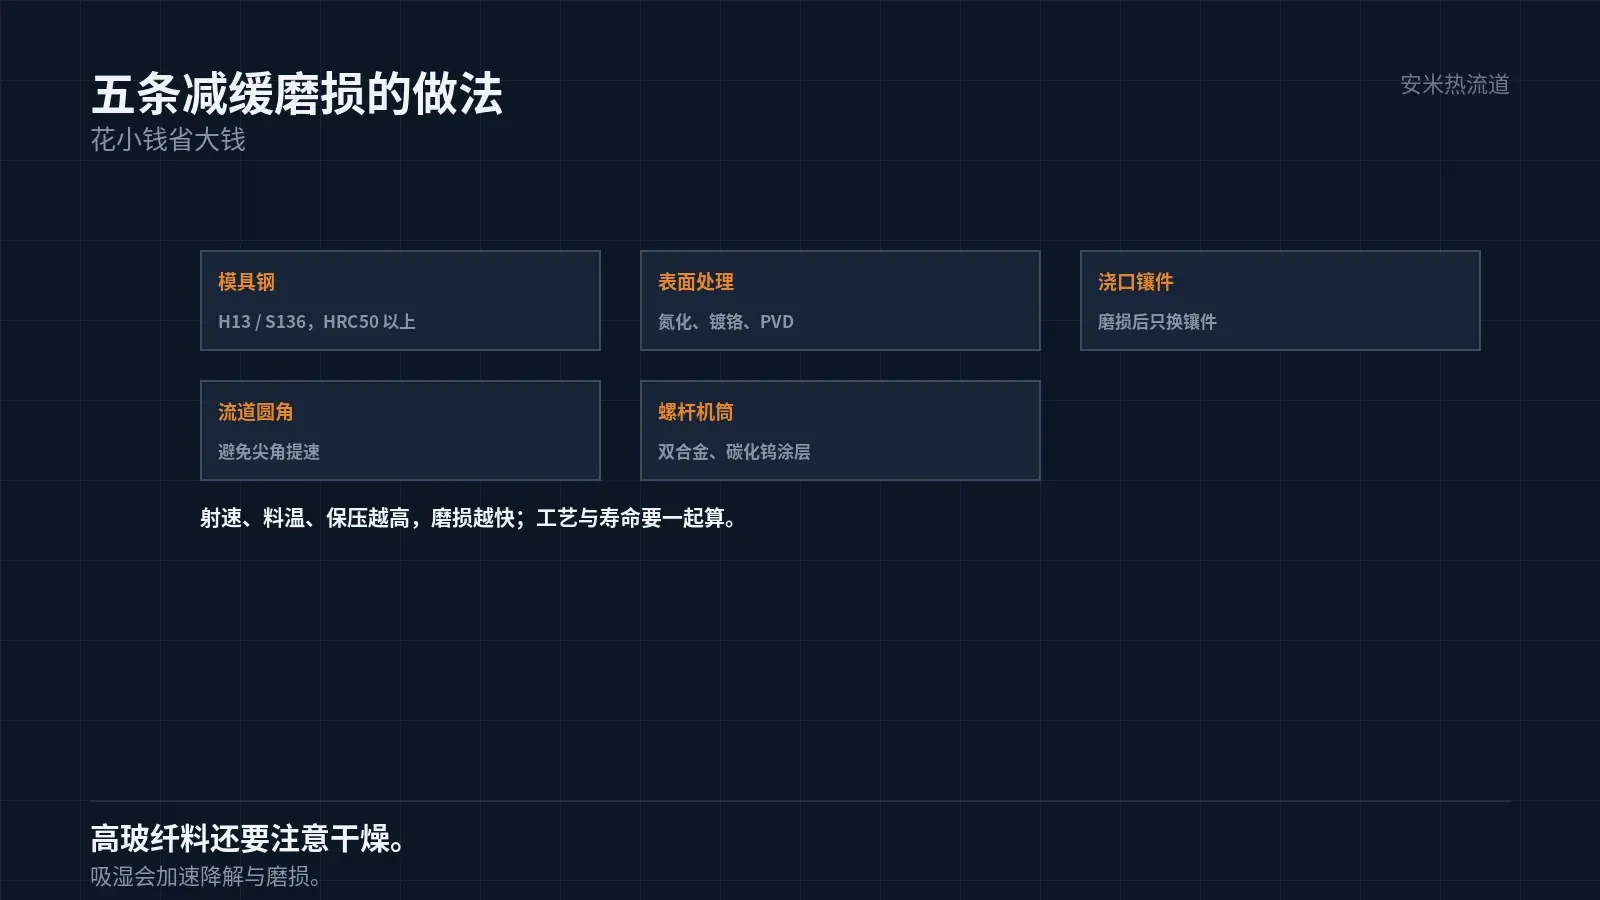
Relationship between wear and process
Higher injection speeds increase flow velocity and accelerate wear. For high glass-fiber materials, balance filling requirements against wear.
Higher melt temperatures reduce viscosity and increase flow rate, accelerating wear. Avoid unnecessarily high temperatures.
Higher holding pressure raises gate pressure and accelerates wear. Set holding pressure according to actual part requirements; avoid over-setting.
These three parameters address the previously discussed filling and warpage issues. Processing high-glass-fiber parts requires balancing multiple objectives.
Process engineers must understand: increasing injection speed to fix short shots reduces mold life. Clarify this trade-off with customers.
Another variable is glass fiber length. Long fibers are more abrasive but provide higher strength. Consider these factors during material selection.
Long glass fibers are harder to process due to poor flow and difficult dispersion. Not all parts are suitable for long glass fiber reinforcement.
Acceptance and Maintenance
Group 1: Record gate dimensions, part weight, and appearance for first articles from new molds. Group 2: Re-measure every 50,000 cycles to monitor changes. Group 3: Replace inserts when wear reaches limits.
Completing this record clarifies the mold life curve and eliminates guesswork about replacement timing.
Records must include material grade, glass fiber content, injection speed, and melt temperature. Changing materials alters the life curve and requires a new baseline.
Please provide the material grade, glass fiber content, mold material, current injection speed, and shot count. We will verify wear and process parameters before providing a quote.
MATCHED BY MATERIAL AND DEFECT
This article covers surface gating or small precision parts; check TP for gate position and whether a dot mark is acceptable.
Register for a selection review and quote
Submit part, mold, and material details. Our engineers will evaluate the gate solution per part and provide a quote.
Upload a 2D layout drawing using the form.
Online selection and quote
Scan to register