
PEEK Compressor Seals Leaking After Three Years: Why?
Material Applications16 min read
On this page
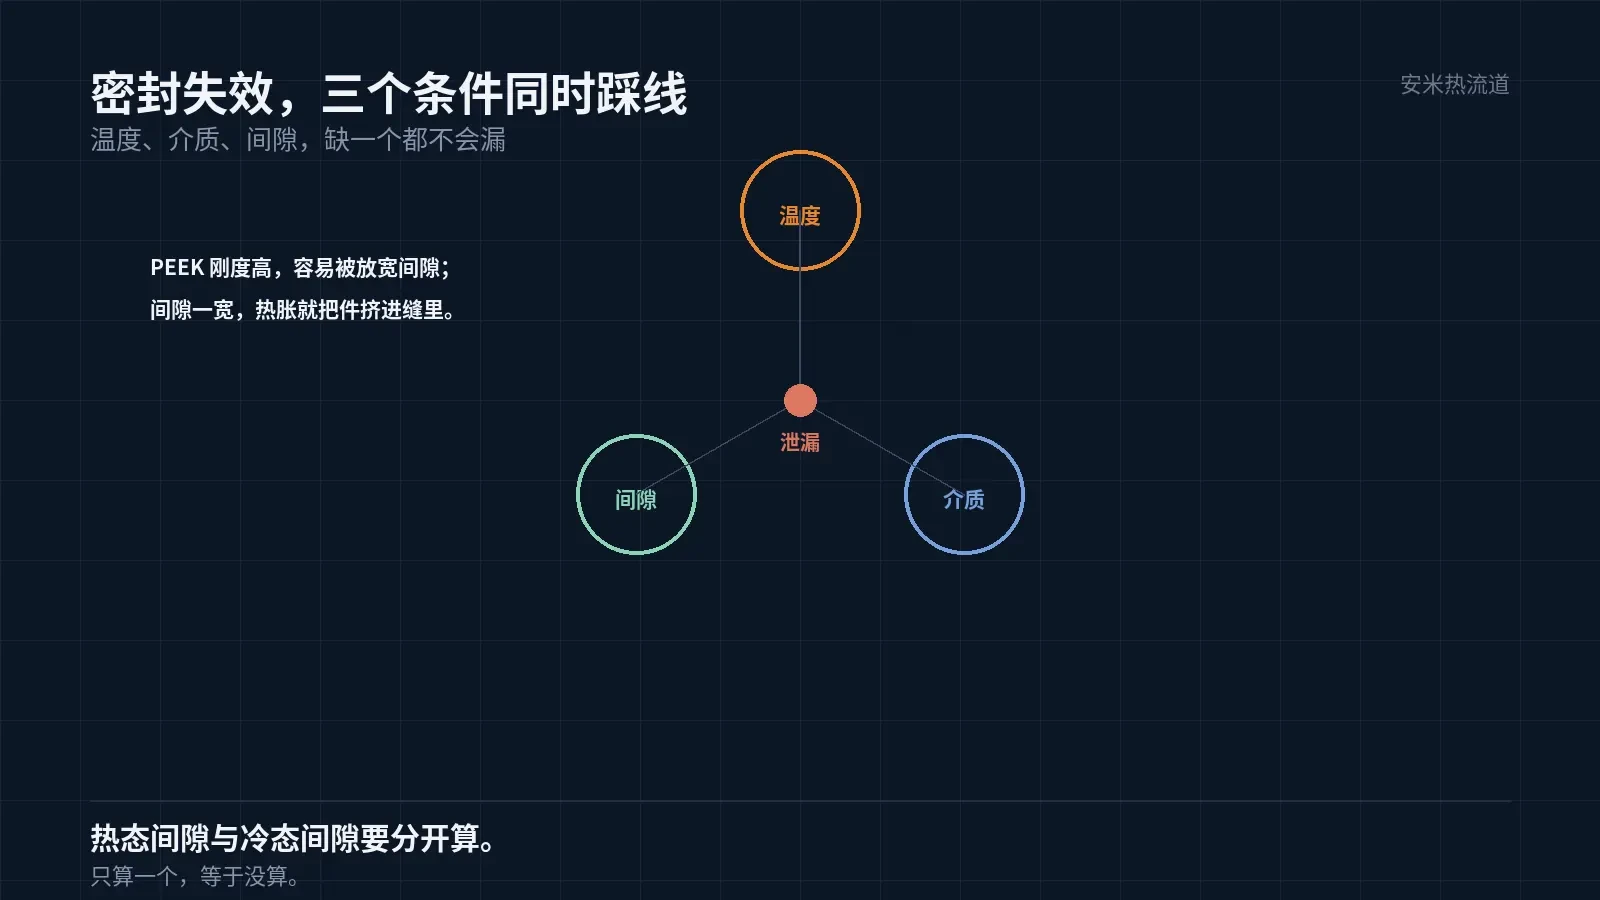
Industrial seal failures are rarely caused by "material incompatibility." Most result from three conditions occurring simultaneously: temperatures near the upper limit, aggressive media, and incorrect clearance calculations. PEEK's high strength and heat resistance often lead designers to increase clearances.
This article covers PEEK seals in compressors, pumps, and valves: their advantages, reasons for premature failure, and methods to independently verify the three critical conditions.
PEEK offers high stiffness but lacks elasticity.
A seal's primary function is conformability. High-modulus materials like metal and PEEK rely on machining precision and preload for sealing, not inherent elasticity. Once clearance changes, they cannot self-compensate.
Therefore, PEEK seal failures are typically not due to wear but rather "displacement": as temperature rises, parts expand and clearances shrink, leading to extrusion; as temperature drops, parts contract and clearances widen, causing leakage.
This explains why PEEK seals of the same grade can have service lives that vary by several times across different equipment. The difference stems from clearance and thermal expansion matching, not the material itself.
During design, calculate PEEK's coefficient of thermal expansion, equipment thermal expansion, and assembly tolerances in a single table. If calculations are not feasible, determine clearance through testing instead of relying on empirical rules.
Temperature: 343°C is the melting point, not the operating temperature.
PEEK has a melting point of 343°C and a long-term service temperature around 250°C, depending on the grade. While this suggests ample margin, seal component temperatures reflect friction surface temperatures rather than ambient conditions.
Local temperatures at friction surfaces can exceed the bulk temperature by tens of degrees, especially under dry or semi-dry friction. Surface blackening and blistering indicate localized overheating.
Temperature analysis must be based on friction surface conditions, not medium temperature. If calculation is difficult, embed thermocouples for direct measurement as the most efficient solution.
Temperature also affects medium erosion rates. For the same medium, a 20°C increase can double the erosion rate. Both factors must be evaluated together.
Medium: Chemical resistance charts only exclude; they cannot confirm.
PEEK resists most media but fails against strong oxidizers like concentrated sulfuric and nitric acids. Sample charts are broad and suitable only for excluding clearly incompatible options, not for confirmation.
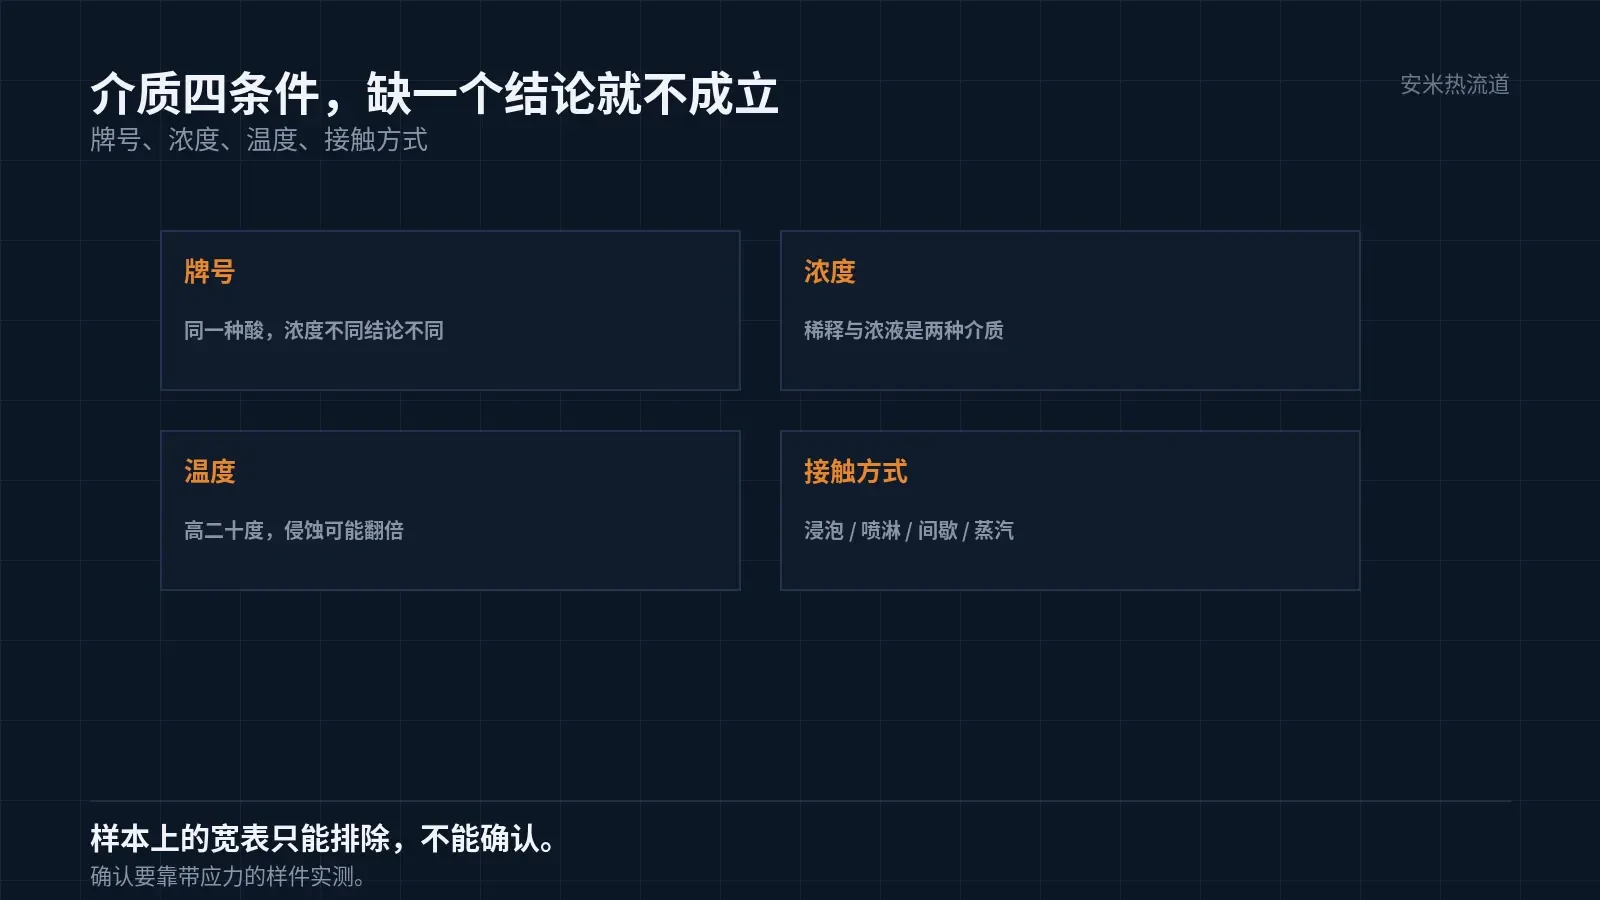
Confirmation requires four parameters: medium grade, concentration, temperature, and contact mode. Contact modes include immersion, spray, intermittent, and steam, each with distinct pressure profiles.
Compressor media often consist of multi-component mixtures including lubricant, refrigerant, and moisture. Erosion in mixed media is more complex than in single media and requires actual testing.
Testing must use samples under actual stress, not flat specimens. Seals experience preload and medium pressure during operation; these stresses accelerate crack propagation.
Downtime is another factor. During shutdowns, media stagnation leads to temperature drops, component shrinkage, and gap changes. Upon restart, medium pressure forces components back into position. Repeated start-stop cycles cause more damage than continuous operation.
Clearance: The Most Common PEEK Pitfall
PEEK's high stiffness often leads designers to widen clearances, assuming it won't extrude. This is a common mistake.
With increased clearances, sealing surface contact depends on preload. As temperature rises, PEEK expands and consumes the clearance; parts are forced into the gap, leading to edge shear failure. As temperature drops, the clearance increases again, separating the sealing surfaces and causing leakage.
The correct approach is to calculate thermal expansion based on operating temperature, defining both "hot" and "cold" clearances. Both values must be within acceptable limits; calculating only one is insufficient.
Glass-filled grades exhibit lower thermal expansion and higher stiffness but are brittle. Unreinforced grades offer better toughness but higher expansion. Selecting a grade directly determines whether clearance calculations can be accurate.
Molding: PEEK has a narrow processing window
Nozzle at 395°C, barrel zones at 375/380–385/390°C, and mold temperature at 170–200°C. This tight range requires capable equipment: barrel heating must reach 400°C, while HT and ST require 430°C.
Dry at 120–150°C for 3–5 hours. Although PEEK has low moisture absorption, its high processing temperature can cause vaporization at the nozzle if moisture remains, creating bubbles. Bubbles in seal components may lead to leaks.
Shrinkage: Unreinforced 0 max/1.3%; with 30% glass fiber 0.30%/0 max. Seal components require high dimensional accuracy; grades with higher shrinkage must be controlled via mold temperature and holding pressure.
Gate selection based on company records: SD, VG, and PVG are acceptable for PEEK; TP is not. Most seals are ring-shaped; gates must avoid sealing surfaces, and weld lines must not occur in mating areas.
Validation: Run three operating conditions simultaneously
Temperature cycling, pressure cycling, and media immersion must be performed together. Testing any single condition alone will not reveal failures such as yielding.
The test bench must control temperature, pressure, and media switching simultaneously. If not possible, perform combined temperature and pressure cycling first, followed by separate media immersion testing.
Define failure criteria in advance: leakage rate, dimensional change, and surface condition. Exceeding limits for any of these three constitutes a failure; do not wait for visible leakage.
Please provide equipment operating conditions (temperature, pressure, media, clearance), part drawings, current material, and service life. We will evaluate each condition separately and issue a quotation once the solution is confirmed.
MATCHED BY MATERIAL AND DEFECT
This article covers stringing, drooling, clogging, and high-heat resins; refer to SD for gate freeze and break-off.
Register for a selection review and quote
Submit part, mold, and material details. Our engineers will evaluate the gate solution per part and provide a quote.
Upload a 2D layout drawing using the form.
Online selection and quote
Scan to register