
Uneven Gloss: Why One Part Has Both Shiny and Matte Areas
Injection Molding Encyclopedia8 min read
On this page
On the same part, some areas are glossy while others are matte, with a distinct boundary that cannot be smoothed out by mold polishing. This is uneven gloss.
This article clarifies whether gloss differences originate from mold temperature, surface finish, or packing pressure, and explains how to distinguish them from flow marks and color variations.
1. Location
The glossy-matte boundary on the same part often coincides with cooling channel layout, flow path, or insert boundaries.
Gloss differences can also occur between cavities in the same mold, related to cavity-specific mold temperatures and gate locations.
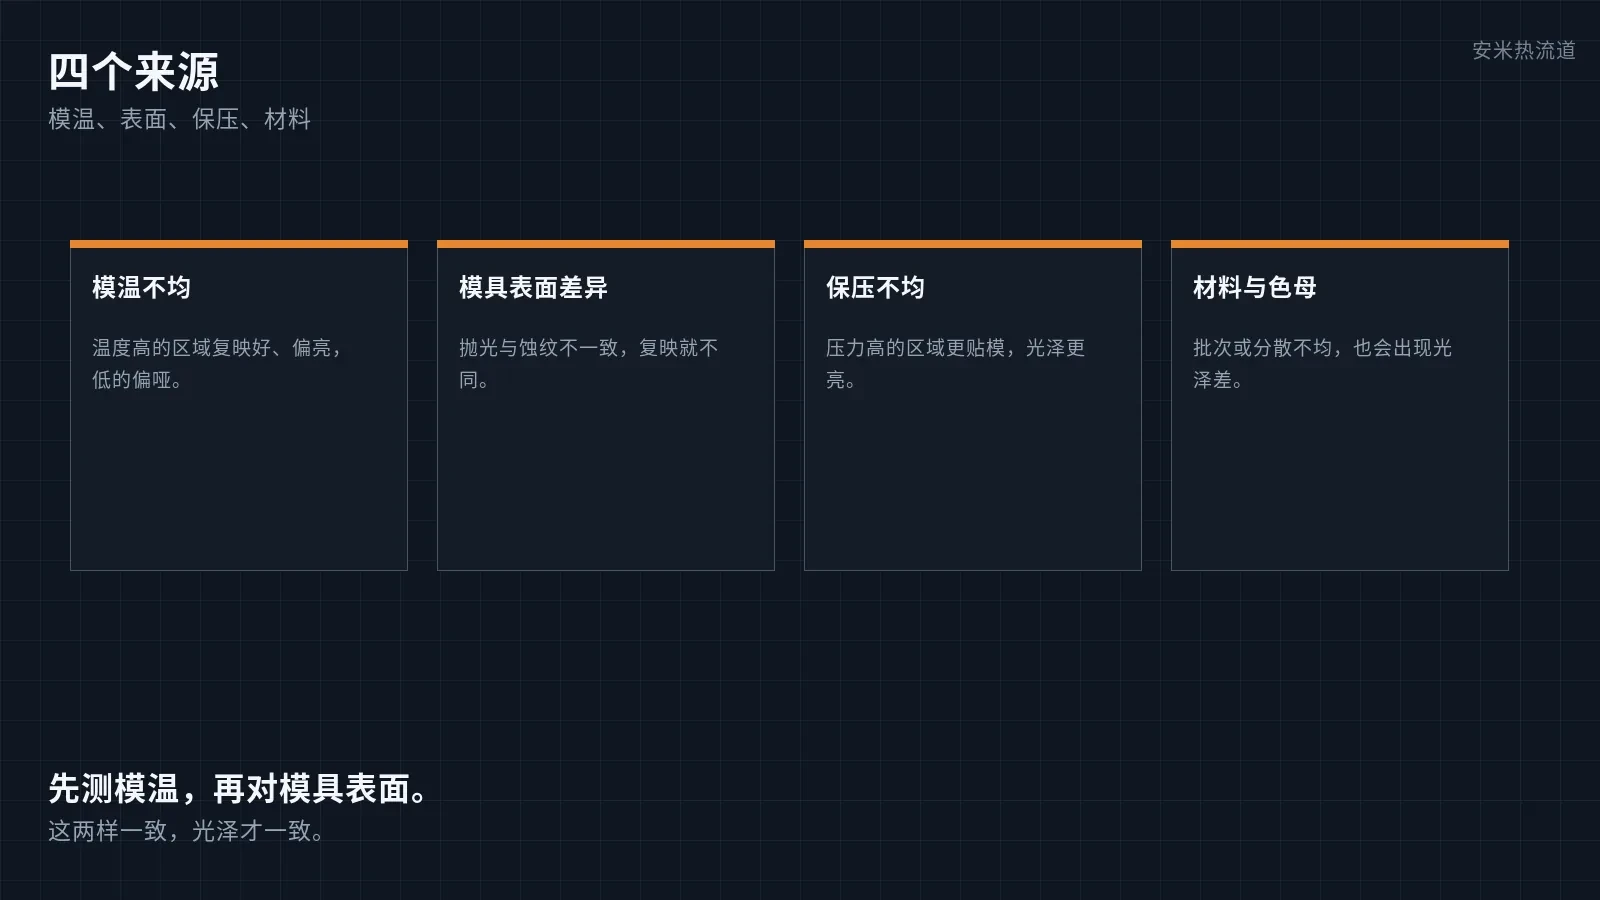
2. Root Causes
Uneven mold temperature: Areas with higher temperature allow better melt contact with the mold wall and clearer replication, resulting in a glossier appearance; lower temperature areas appear more matte.
Mold surface variations: Inconsistencies in polishing, texturing, or mold repair direction lead to different replication results on the same part.
Uneven holding pressure: Areas under higher pressure adhere more tightly to the mold, resulting in higher gloss.
Material and masterbatch: Uneven dispersion or batch variations can cause surface scattering differences.
Uneven cooling: Blocked water channels or insufficient flow cause localized temperature spikes.
III. Distinguishing Flow Marks from Color Variation
Flow marks are wavy traces with a clear flow direction.
Color variation refers to actual color differences; gloss may remain consistent.
Gloss unevenness is a difference in brightness/darkness; color may be consistent, becoming more apparent at different viewing angles.
IV. Responsibility allocation
Mold aspect: Cooling channel layout and flow rate; consistency of cavity surface treatment.
Injection Molding Machine: Hold Pressure and Mold Temperature Controller Settings
Hot runner aspect: Temperature consistency across cavities to avoid one cavity appearing glossier.
5. Solutions
Measure mold temperature point by point to identify the area with the largest temperature difference; prioritize cooling water circulation before addressing other factors.
Standardize cavity surface treatment to ensure consistent polishing direction and texture depth per specification.
Balance holding pressure; verify per cavity in multi-cavity molds.
Implement zone temperature control with individual settings for each cavity to prevent variations between glossy and matte finishes.
Clarify boundaries: Gloss variation is not color variation, so masterbatch adjustment will not resolve it; nor is it due to dirty mold surfaces, as cleaning only removes stains, not temperature differences.
Conclusion
Poor gloss is due to poor surface replication. Gloss consistency requires the mold temperature to match the mold surface.
For further verification, please provide the mold 2D layout drawing. We will check gate and cavity temperatures item by item based on the layout, then confirm the solution and quotation.
MATCHED BY MATERIAL AND DEFECT
The article covers gate marks or residue on cosmetic surfaces; check VG for a flush break and pin maintenance.
Register for a selection review and quote
Submit part, mold, and material details. Our engineers will evaluate the gate solution per part and provide a quote.
Upload a 2D layout drawing using the form.
Online selection and quote
Scan to register