
Air Traps and Entrapped Air: Issues at the Last Fill Point
Injection Molding Encyclopedia7 min read
On this page
Burn marks, short shots, bubbles, or trapped air consistently appear at the same locations: part ends, weld lines, and deep cavity bottoms. This is caused by air traps and gas entrapment.
This article clarifies where gas is trapped, how to distinguish it from silver streaks and burn marks, and why venting must be addressed before adjusting gate temperature.
1. Defect Location
Last fill points: Ends, corners, and deep cavity bottoms where gas is pushed by the melt with no escape path.
Weld lines: Gas is trapped between converging flow fronts, forming gas trap marks.
Rib and boss ends: Thin structures and confined spaces make these areas prone to gas retention.
2. Root Causes
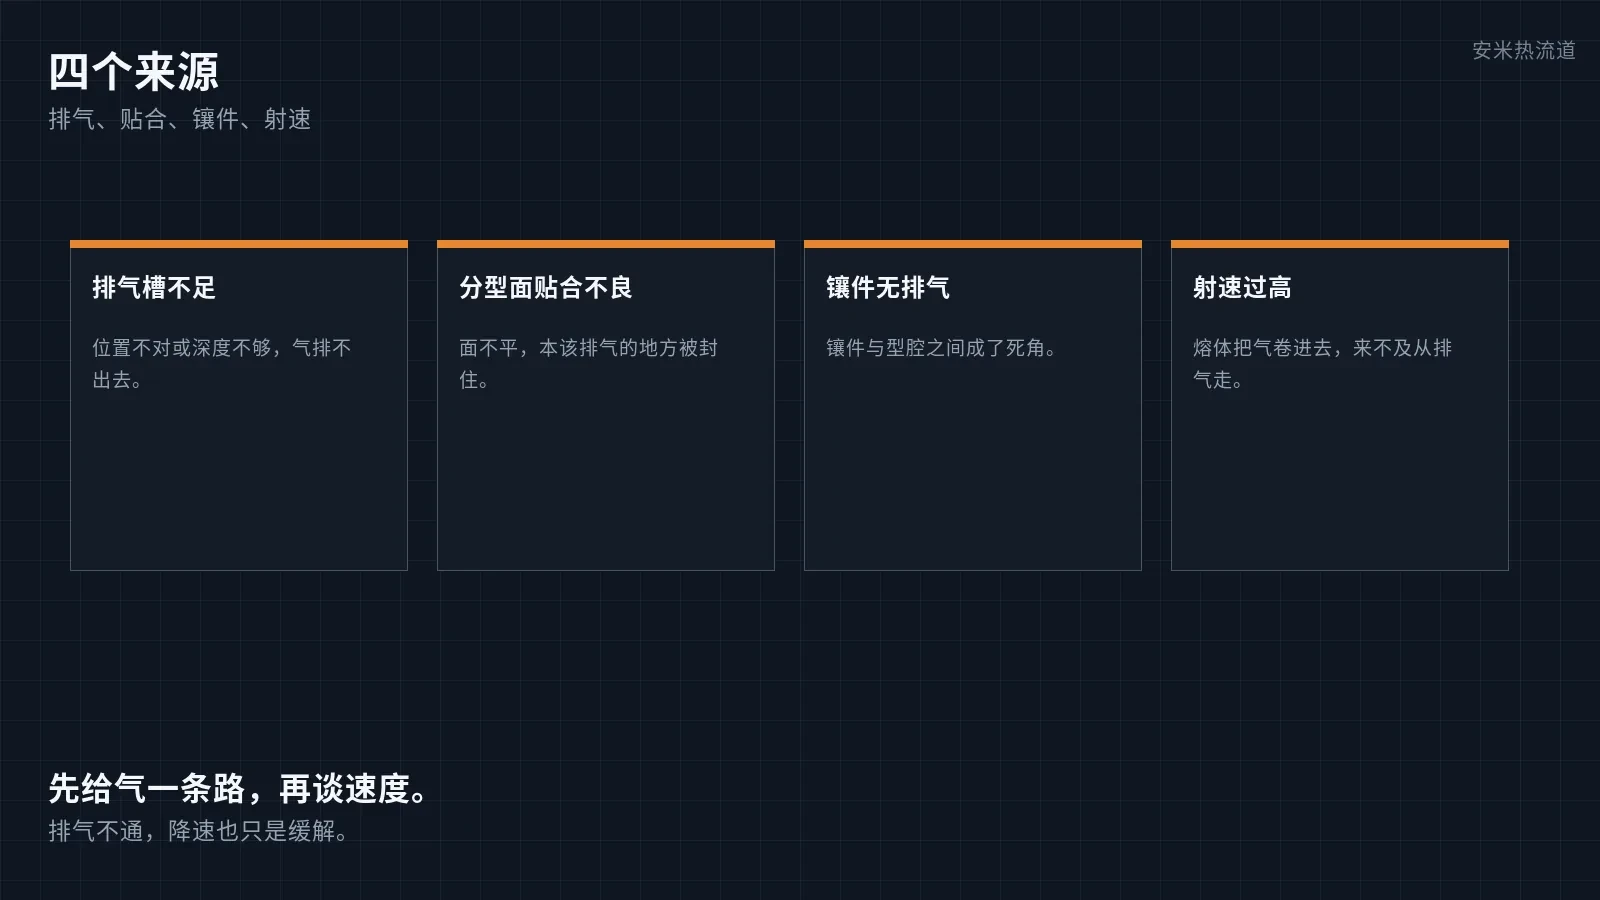
Insufficient vent groove location and depth: No vents at critical areas, or vents are too shallow.
Poor parting line fit: Deformation or foreign matter on the surface blocks air from escaping through the gap.
No venting at inserts and ejector pins: Fitting clearances form closed dead zones.
Injection speed too high: Melt front traps air, exceeding venting capacity.
Unreasonable gate location: The end of the flow path is too far from vent points, trapping air in unvented areas.
III. Distinguishing from silver streaks and burn marks
Silver streaks are silvery-white stripes caused by moisture and gas near the gate, with widespread distribution.
Burn marks result from high-temperature carbonization of compressed gas, appearing dark brown to black and recurring at the same location.
Air traps are short shots, bubbles, or sink marks left by trapped air, fixed at the end of the flow path.
4. Responsibility Allocation
Mold features: Venting grooves and insert vents, parting line fit, cavity surface finish.
Injection Molding Machine: Injection Speed Profile and Back Pressure
Gate and hot runner considerations: Gate location and flow length determine the final fill point.
5. Solutions
Machine venting grooves at the last fill point and weld lines; depth depends on material viscosity.
Check the parting line fit and insert mating surfaces; add venting inserts if needed.
Use staged injection speeds with deceleration at the end to allow air to escape through vents.
Use mold flow analysis to confirm the final fill point and position vents correctly.
Clarify boundaries: Hot runner heating cannot replace venting. Do not adjust gate temperature until air is fully evacuated from the first five stages.
Final Notes
Gas marks are an air issue, not a material issue. Proper vent placement prevents repeated burn marks at the end of the fill.
For further verification, please provide the 2D mold layout drawing. We will review gate and cavity temperatures against the layout item by item before providing a solution and quotation.
MATCHED BY MATERIAL AND DEFECT
This article covers surface gating or small precision parts; check TP for gate position and whether a dot mark is acceptable.
Register for a selection review and quote
Submit part, mold, and material details. Our engineers will evaluate the gate solution per part and provide a quote.
Upload a 2D layout drawing using the form.
Online selection and quote
Scan to register